10 Ton Annealing Furnace for Steel Wire Coils
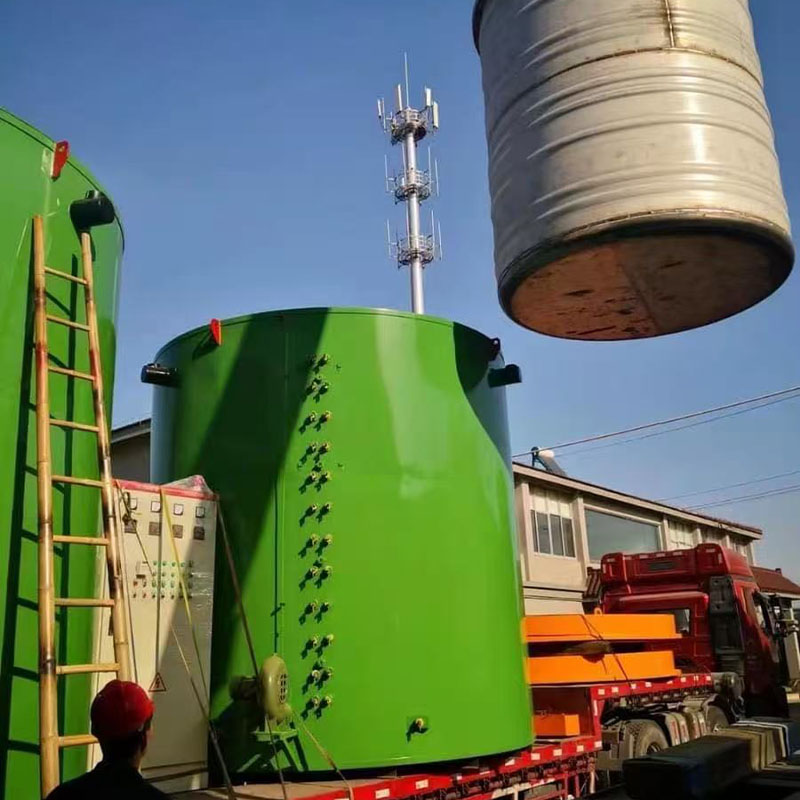
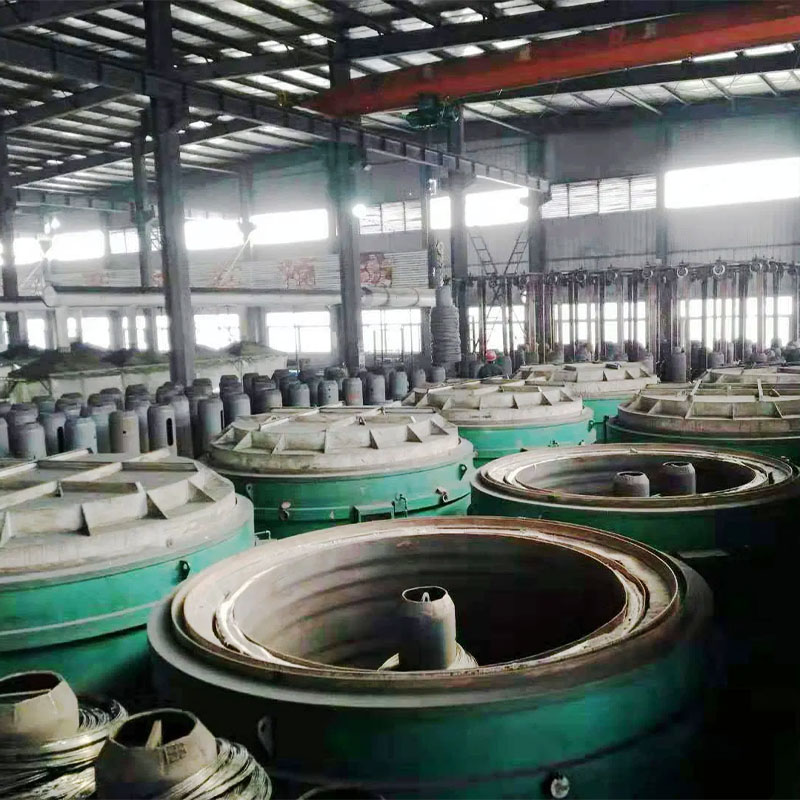
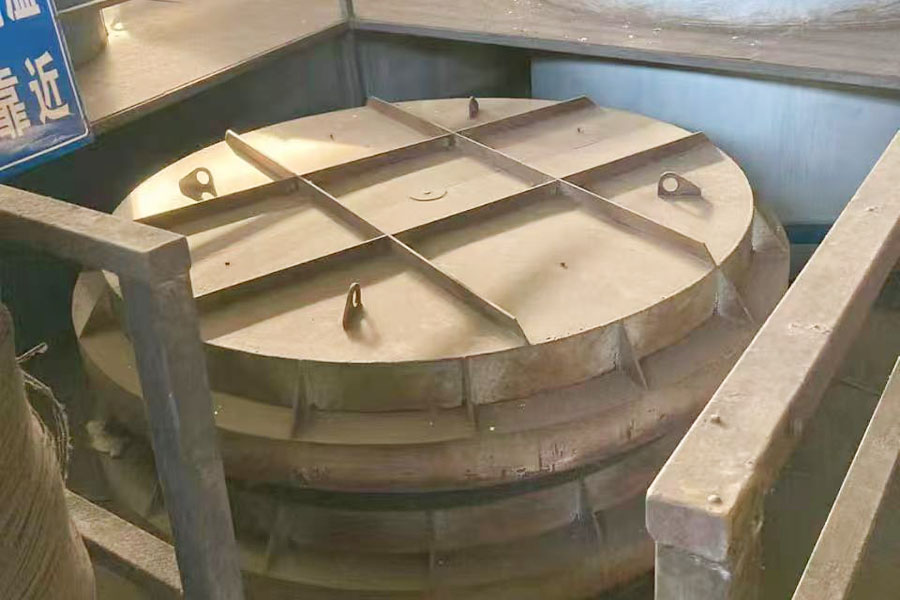
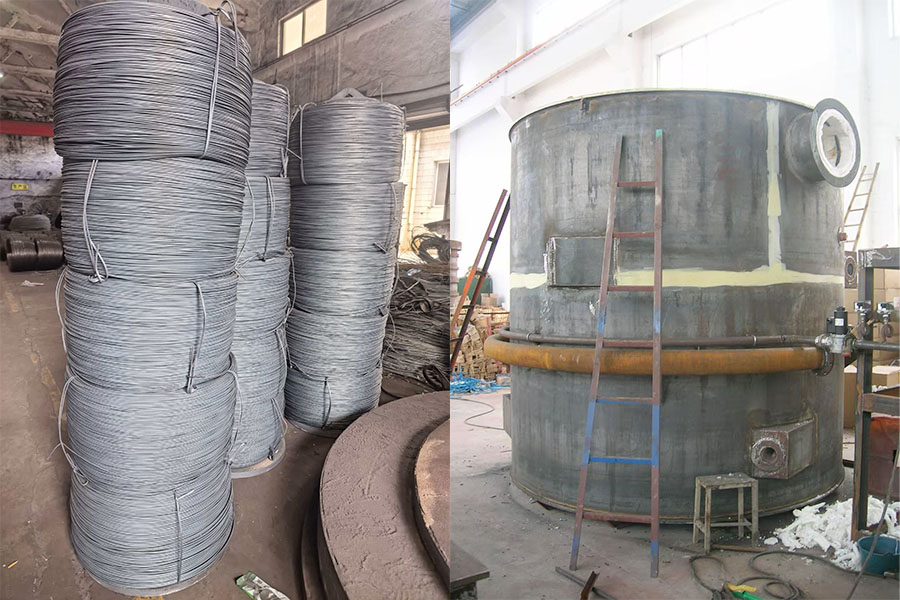
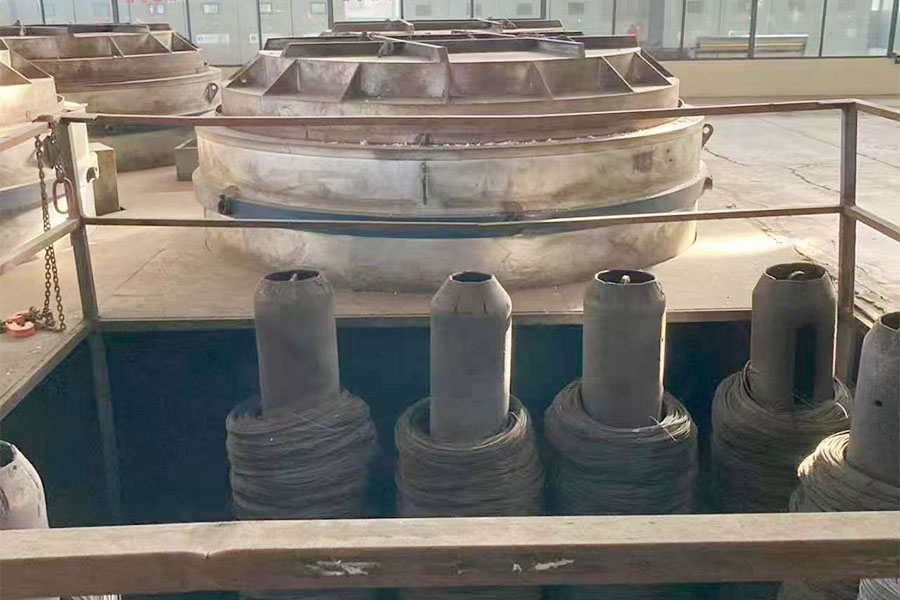
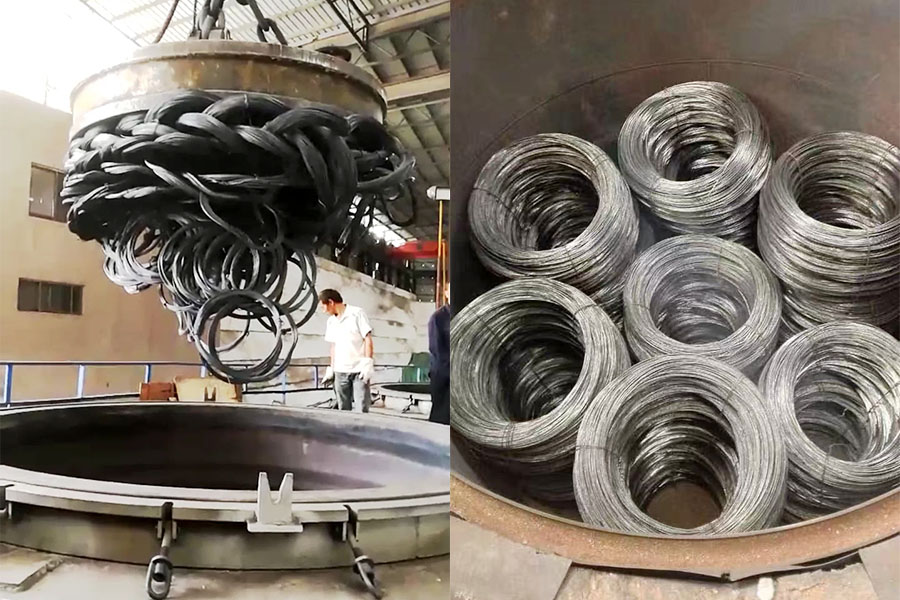
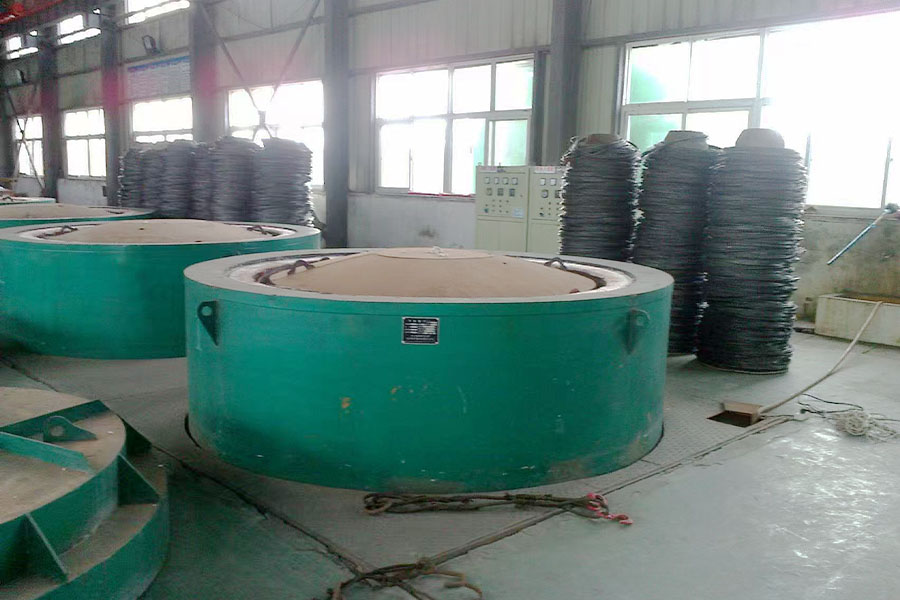
YF Metal Tech designs and manufactures this 10-ton annealing furnace (well-type annealing furnace) for the gas-protective annealing of low-carbon (mild) steel wire coils. Five coil stacks, each φ750 mm in outer diameter, 2,200 mm high and about 2 tons in weight, load into the furnace in a single batch of up to approximately 10 tons. A top-mounted 11 kW convection fan circulates the atmosphere through a corrugated guide cylinder, and three independently controlled temperature zones hold the charge at 680–720 °C with ±2 °C control accuracy.
Key Features
|
Parameter |
Specification |
|---|---|
| Application | Gas-protective annealing of mild (low-carbon) steel wire coils |
| Charge per batch | Up to approx. 10 t (5 stacks × approx. 2 t) |
| Coil size per stack | φ750 mm OD × 2,200 mm high |
| Working temperature | 680–720 °C (maximum service temperature 850 °C) |
| Heating | Electric, 320 kW, 380 V / 50 Hz, Cr20Ni80 resistance band |
| Temperature control | 3 zones (upper / middle / lower), PID touch-screen cabinet, ±2 °C accuracy |
| Temperature uniformity | ±5 °C (late holding stage) |
| Atmosphere | Nitrogen protection, or black annealing without gas |
| Circulation | 11 kW convection fan, 11,000 m³/h, 1,600 Pa |
| Cooling | Furnace cooling, then air cooling with 3 × 3.0 kW fans |
Why Anneal Drawn Steel Wire?
Every pass through a wire drawing machine work-hardens the steel: strength rises while ductility falls. Left untreated, heavily drawn low-carbon wire becomes too hard to draw further or to cold-form into nails, screws and other fasteners. Annealing heats the coils above the recrystallization temperature, so new, strain-free grains replace the deformed structure and the wire softens again.
This 10 ton annealing furnace works at 680–720 °C, just below the lower critical temperature (A1, about 727 °C) of carbon steel. That window is a common route for recrystallization (softening) annealing of low-carbon wire, and it also covers the subcritical spheroidizing cycles used to improve cold-heading wire. Hold times and cooling rates depend on your steel grade, wire diameter and coil size; our engineers help you set the process curve that the PID controller then runs automatically.
Protective Atmosphere vs. Black Annealing
With nitrogen protection, air is purged from the sealed inner container before and during heating, so the coils come out with a much cleaner surface than in open-air annealing. When appearance is not critical, for example black annealed tie wire, the same furnace runs black annealing with no gas fill.
Surface quality in protective-gas annealing also depends on coil cleanliness (residual drawing lubricant), nitrogen purity and seal condition. That is why the flange carries a water-cooled silicone seal ring, and why the furnace cover is fitted with a pressure gauge and a stainless pressure-relief check valve.
Where This 10 Ton Annealing Furnace Is Used?
- Nail wire: softening low-carbon wire between drawing passes and before nail forming on a nail making machine.
- Tie wire and black annealed wire for construction and binding.
- Wire for galvanizing, fencing and mesh, where soft, uniform wire is required.
- Cold-heading and fastener wire, where softening or spheroidizing improves formability.
- Wire drawing plants that need intermediate annealing between draws, paired with a low carbon steel wire drawing machine.
How a 10-Ton 10 Ton Annealing Furnace Batch Runs, Step by Step?
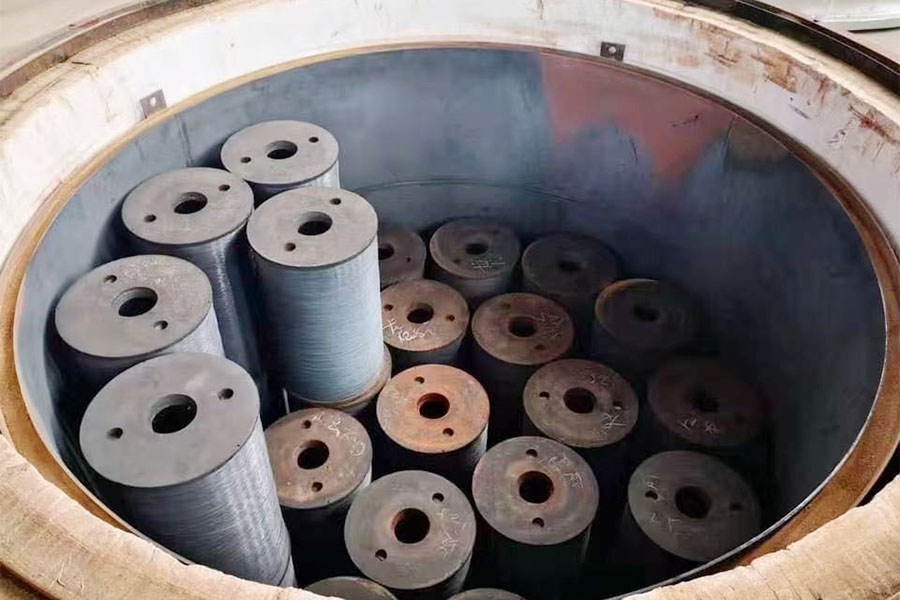
- Load. Coils are stacked on the five loading racks, and a crane lifts the five stacks into the guide cylinder.
- Seal and purge. The furnace cover closes and locks electrically, circulating cooling water is connected, and nitrogen is filled while the air is discharged at the same time.
- Circulate. The forced-convection fan starts, with nitrogen protection continuing.
- Heat and hold. The controller completes heating and holding automatically along the preset process curve.
- Cool. After holding, heating is switched off and the charge furnace-cools for about 2 hours; the cooling fans then start for air cooling.
- Shut down services. Once the charge reaches the temperature set in the process, the cooling fans, convection fan, circulating water and nitrogen are switched off.
- Unload. The cover lock is released, the cover lifts electrically, and the stacks are lifted out.
For black annealing, no gas fill is needed.
Technical Specifications of 10 Ton Annealing Furnace
| Item | Parameter |
|---|---|
| Inner container inner diameter | φ2,400 mm |
| Guide cylinder inner diameter | 2,200 mm |
| Loading height | 2,200 mm |
| Maximum service temperature | 850 °C |
| Working temperature | 680–720 °C |
| Heating power | 320 kW (380 V, 50 Hz) |
| Temperature control zones | Upper, middle and lower zones in the inner container, controlling 3 groups of heating elements |
| Temperature control accuracy | ±2 °C |
| Furnace temperature uniformity | ±5 °C (late holding stage) |
| Shell surface temperature rise | 35 °C above room temperature |
| Cooling fans | 3.0 kW × 3 |
| Convection fan power | 11 kW (4-pole) |
| Convection fan speed | 1,460 r/min |
| Air volume | 11,000 m³/h |
| Fan pressure | 1,600 Pa |
| Impeller diameter | φ600 mm |
| Charging capacity per batch | Max. approx. 10 t |
| Required crane lifting height | ≥ 7.0 m (if lower, the user can excavate a pit) |
Engineering Details
1. Furnace Body and Heating
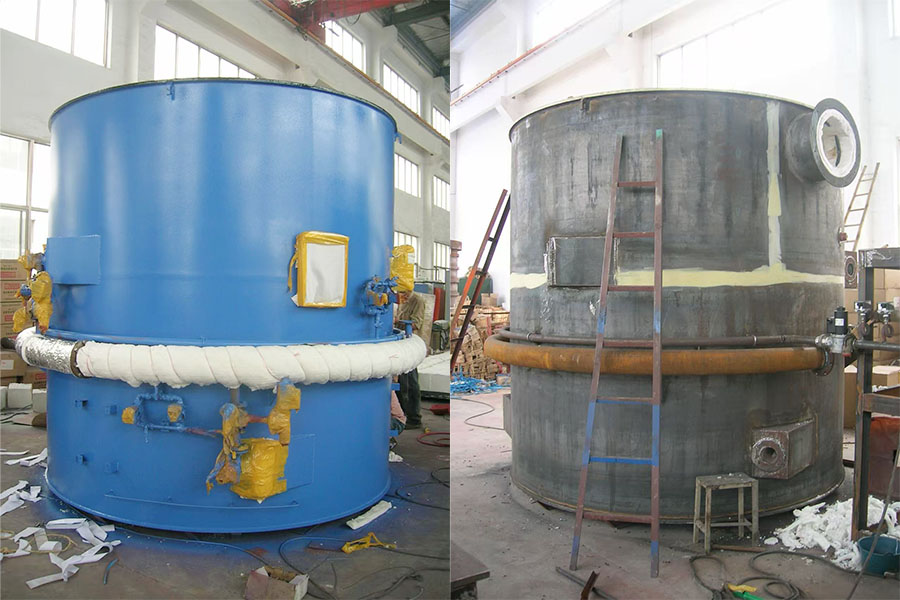
The shell is a 6 mm Q235 steel structure with a flanged top and positioning support plates below. The panel is 20 mm Q235 plate with a stop ring and sealing groove, and the base plate is 12 mm Q235 reinforced with welded I-steel. The wall lining is 250 mm of extruded high-temperature aluminum silicate ceramic fiber modules, fixed to anchors welded on the shell and covered inside and out with a 25 mm layer of high-temperature ceramic fiber blanket. The furnace bottom is insulated with thermal insulation bricks, topped with light refractory bricks.
Heat comes from Cr20Ni80 nickel-chrome flat resistance bands, formed in a wave shape and locked onto the furnace wall with high-temperature ceramic screw nails, 320 kW in total. The side of the furnace body carries the thermocouples, resistance-band lead rods, copper splints and protective cover, plus an electric cover-lifting device with stroke protection, transverse manual operation and a positioning device.
An annular air duct with three 3.0 kW medium-pressure fans sits at the lower outer side of the furnace. Evenly spaced outlet pipes blow air from bottom to top, and ten outlet pipes with flexible cover plates at the top release it. The fans start and stop automatically through the programmed temperature controller.
2. Corrugated 309S Inner Container
The cylinder is 8 mm 309S stainless steel, pressed into corrugations with a 150 mm pitch and 10 mm wave depth. The hot-pressed flat bottom head is 14 mm 309S, and a flow-guiding structure of 200 × 12 mm and 80 × 12 mm 304 flat steel with angle-weld reinforcement gives a bearing capacity of 15 t. The machined 40 mm Q235 upper flange joins the furnace body’s soft-seal positioning ring and the cover locking device, with a sealing groove and a water-circulation-cooled silicone seal ring. Three armored thermocouples with protective devices control the upper, middle and lower zones independently, and the container has lifting lugs.
3. Corrugated 304 Guide Cylinder
The guide cylinder is 6 mm 304 stainless steel with the same 150 mm / 10 mm corrugation. Stainless round-steel turnbuckles and evenly spaced limit support plates at the top and bottom reinforce it, and it directs the circulating atmosphere through the coils. A lifting lug sits at the top.
4. Furnace Cover and Convection Fan
The 10 ton annealing furnace cover has a machined 30 mm Q235 flange welded to a 12 mm Q235 arch head. The lower arch insulation layer and jack cap are 6 mm 309S, filled with aluminum silicate blanket. An 11 kW convection fan with thermistor overheating protection is mounted at the center; its φ600 mm impeller and main shaft are 310S heat-resistant stainless steel on imported bearings, and a 6 mm 309S arched deflector plate sits below it. The cover also carries a cooling water jacket that protects the silicone seal ring, an exhaust pipe valve, three exhaust ports in the insulation layer, a pressure gauge, a stainless pressure-relief check valve and a furnace temperature detection hole.
5. Loading Racks
Five racks, each with a φ750 mm base plate of 20 mm Q235 welded to a φ351 × 8 mm central riser. Vent holes in the plate and riser let the atmosphere reach every stack, and a lifting lug tops each riser.
What Is Included?
|
Item |
Qty. |
|---|---|
| Heating furnace body (with cooling fans and electric lifting device) | 1 set |
| Stainless steel corrugated inner container | 1 set |
| Stainless steel corrugated guide cylinder | 1 set |
| Furnace cover (with convection fan) | 1 set |
| Loading rack (set of 5 pieces) | 1 set |
| PID touch-screen electric control cabinet (packed in a wooden box for export) | 1 set |
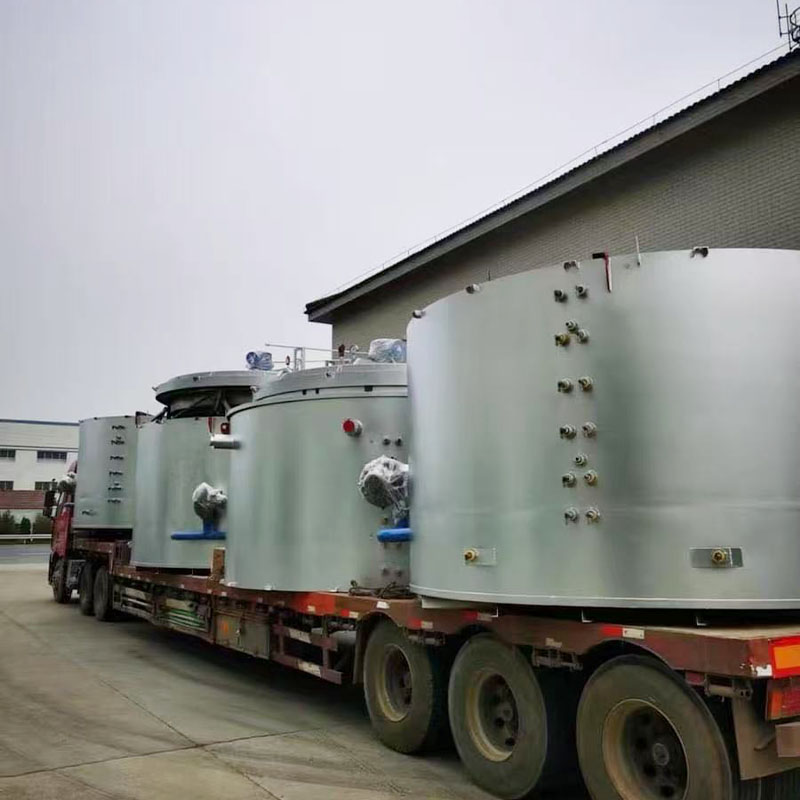
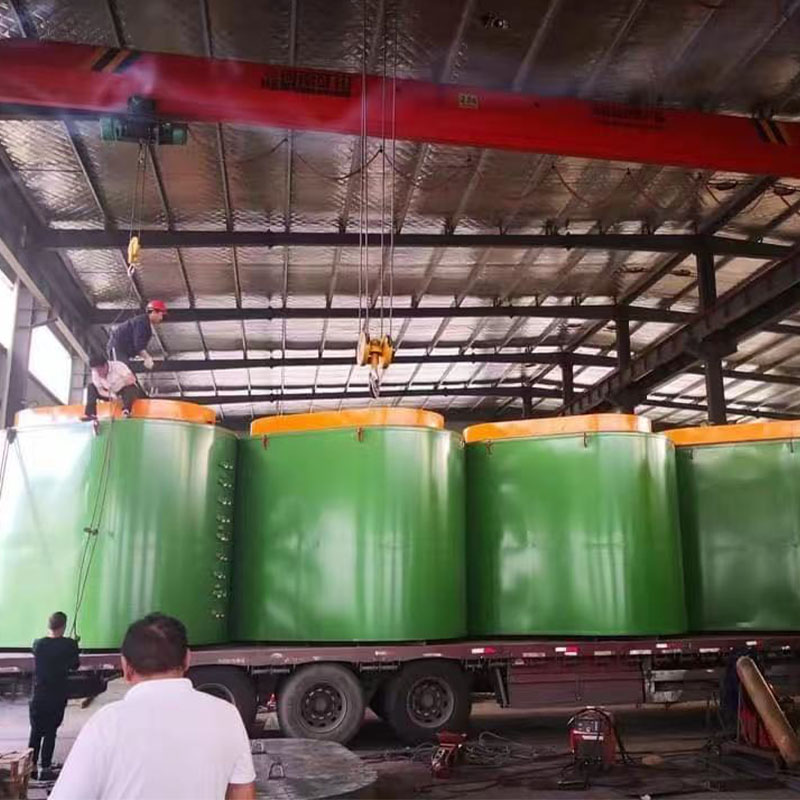
| Export packing and fixing for container shipment (tarpaulin, binding tape, etc.) | 1 set |
How to Choose a 10-Ton Annealing Furnace?
Send us these five details and we will confirm the configuration and the process curve:
- Coil size and weight: outer diameter, inner diameter, stack height and weight per coil. This furnace takes stacks of φ750 mm × 2,200 mm at about 2 t.
- Steel grade and wire diameter, plus the hardness or tensile strength you need after annealing.
- Atmosphere: nitrogen protection or black annealing, and whether nitrogen is available on site.
- Throughput: annual tonnage or batches per day, so we can tell you whether one furnace is enough.
- Site conditions: grid voltage and frequency, cooling water supply, and crane hook height (at least 7.0 m, or a pit).
Well-Type vs. Bell-Type Annealing Furnace
Both furnace types anneal wire coils under a protective atmosphere. They differ in how the charge and the heat source are arranged.
|
Well-type (pit-type), this furnace |
Bell-type |
|
|---|---|---|
| Charge handling | Coils are lowered from above into a sealed inner container inside a fixed furnace; the cover carries the convection fan | A heating bell is lifted over coils stacked on a fixed base, under a sealed inner cover with its own circulation fan |
| Batch size | One charge at a time, about 10 t here | Several bases can run in sequence under shared heating bells and cooling hoods |
| Scaling up | Add furnaces as volume grows | Add bases to an existing line |
| Best fit | Moderate annual tonnage of mild steel wire, one robust station | High, continuous tonnage that justifies a multi-base line |
If your volume calls for a multi-base line, tell us. We will say plainly whether one furnace, several of these furnaces, or a different arrangement suits your plant.
Frequently Asked Questions
1. What temperature is used to anneal low-carbon steel wire?
This 10 ton annealing furnace works at 680–720 °C, just below the A1 critical temperature of carbon steel (about 727 °C), and is rated for a maximum service temperature of 850 °C. The exact set point depends on steel grade, degree of cold work and target hardness.
2. How much wire can it anneal per batch?
About 10 tons: five stacks, each φ750 mm × 2,200 mm and approximately 2 t.
3. What is the difference between black annealing and protective-gas annealing?
Black annealing runs without protective gas, so the wire leaves with a dark oxide layer; it suits tie wire and uses where appearance is secondary. Protective-gas annealing fills the sealed container with nitrogen, which largely prevents oxidation. This furnace does both.
4. Why does the furnace use forced convection?
In a sealed container, heat reaches dense wire coils mainly by radiation and conduction from the container wall, so the outer wraps heat faster than the core. The 11 kW fan drives the atmosphere through the guide cylinder and around each stack, which evens out the temperature and supports the ±5 °C uniformity of the late holding stage.
5. How is the charge cooled?
After holding, heating is switched off and the charge furnace-cools for about 2 hours. Three 3.0 kW cooling fans then blow air around the furnace until the charge reaches the temperature set in the process, and the cover is opened for unloading.
6. What do I need to prepare on site?
A crane with a hook height of at least 7.0 m (or a pit excavated by the user if the height is not enough), 380 V / 50 Hz power for the 320 kW heating, circulating cooling water, and a nitrogen supply for protective-gas annealing.
7. Can this furnace anneal stainless steel, copper or aluminum wire?
This model is designed for mild steel wire. For stainless steel wire we build a continuous stainless steel annealing line, and for copper wire we supply copper wire drawing machines with continuous annealing. Tell us your material and we will point you to the right equipment.
8. How much does a 10-ton annealing furnace cost?
The price depends on the configuration: voltage and frequency, atmosphere requirement, control configuration and export packing. Send your coil size, steel grade and site conditions through the form below and we will quote the furnace as a complete set.
9. Do you export, and is the furnace shipped complete?
Yes. YF Metal Tech exports wire drawing machines and auxiliary equipment to Germany, Italy, Spain, Japan, Turkey, UAE, Pakistan, India, Vietnam, Egypt and other countries. This furnace is packed and fixed for container shipment, with the control cabinet in a wooden box.
Why Buy from YF Metal Tech?
- Factory direct, OEM and ODM available: you deal with the manufacturer in Jiangyin, Jiangsu, China.
- Designed around your line: coil size, atmosphere and site conditions set the configuration.
- Tested before delivery: quality control and testing are carried out before shipment.
- One supplier for the whole wire line: wire drawing machines, pay-off and take-up machines, annealing furnaces and nail making machines.
- Fast response and after-sales support for overseas customers.
Request a Quotation for the 10-Ton Annealing Furnace
Tell us your coil size, steel grade, annealing target, voltage and site crane height, and our engineers will reply with a configuration and quotation.
- Email: sarah@yfmetaltech.com, adela@yfmetaltech.com
- WhatsApp: +86 157 9315 9396
- Address: No.151 Shengang Road, Lingang Street, Jiangyin City, Jiangsu Province, China